

 EN

Hot Stamping Foil on UV-Varnished Cartons: What Buyers Should Check
2026/10/28
Gold foil can be stamped on selected UV-varnished cartons, but the surface and foil must match. Learn what to check before approving a finished box.
2026/10/27

2026/10/27
What is hot stamping? In packaging decoration, it is a dry transfer process that uses heat, pressure, and a carrier film to move a thin decorative layer onto a substrate. Unlike ink printing, hot stamping does not soak into paper or film. A heated die or roller presses foil against the surface, the adhesive layer activates, and the release layer lets the decorative film separate from its carrier. The result is a crisp graphic, often with a reflective metal look, holographic pattern, matte color, or pearlescent effect. Packaging buyers ask for it because the decoration sits on top of the surface, so it catches light in a way that ink cannot. It appears on cosmetic cartons, spirits labels, pharmaceutical boxes, consumer electronics sleeves, and on the daily chemical tubes and bottle caps that carry a brand logo. Hot stamping is not one recipe. Every substrate, foil, die, and press combination behaves a little differently.
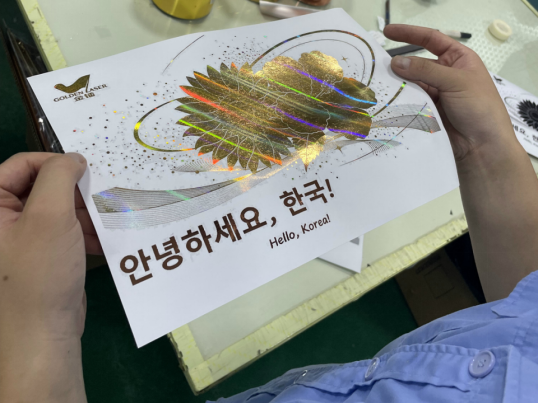
A stamping foil is an engineered sandwich, not a simple sheet of metal. The carrier is a thin film that holds the layers during coating and transfer. A typical metallic foil includes a release coat, a color or protective lacquer, a metallized layer and an adhesive size coat. Pigment and transparent holographic foils use different constructions and need not contain a metal layer. During hot stamping, the heated tool softens the release coat and activates the adhesive. Pressure keeps the foil in contact with the substrate. When the tool lifts, the adhesive holds the decorative layers to the substrate while the carrier pulls away. Temperature matters. Run too cool, and transfer looks patchy or dull. Run too hot, and edges blur, adhesive oozes, or the carrier drags. Substrate chemistry is just as important. Coated papers, treated films, and some smooth surfaces accept foil well. Untreated low-energy films, silicone residues, and heavy UV coatings often fight adhesion. Tape, rub and fold checks after the relevant finishing steps help assess transfer adhesion and durability. Most transfer problems start at the interface, not in the foil roll alone.
Hot stamping equipment falls into a few families, and each changes the recipe. Flatbed presses use a heated platen and vertical squeeze, which suits sheet-fed cartons and labels. Rotary presses use a heated roller and nip, which fits web work and roll labels. Digital foil transfer is a separate route that may use toner or digitally applied adhesive or varnish. Its heat and curing requirements depend on the equipment, and it can support short runs or variable designs without a conventional stamping die. The right choice depends on run length, substrate, graphic detail, and downstream finishing.
Flatbed hot stamping applies a heated die to the substrate and is commonly used for sheet-fed cartons and labels. Check die temperature, make-ready, pressure and dwell time for the specific job.
Rotary hot stamping uses rotating tooling and suits continuous-web work. Web tension, tooling geometry, speed and registration must be matched; pressure is not universally lower than on a flatbed press.
Digital foil transfer uses a compatible digitally generated image, toner, adhesive or varnish system. It is useful for appropriate short-run and variable-design work, but the required foil, curing or heating conditions and achievable finish are equipment-specific.
Dwell, pressure, die material, surface condition and make-ready interact. Paper hot stamping commonly uses metal dies; compliant silicone tooling is used for some other applications. The appropriate tooling depends on the substrate and shape, so there is no universal rule that a harder die needs less pressure. Substrate thickness changes the gap, so a setup that works on one board weight may fail on a heavier one. Good operators record settings by job, not by machine alone, because heat, pressure and dwell time are established through a sample ladder and verified after cooling rather than carried over from another job.
Packaging decoration uses hot stamping when a brand needs depth, reflectivity, or a tactile signal that ink cannot deliver. A cosmetics carton may use a metallic gold from the standard gold and silver range for a logo and a matte series foil for a pattern. A spirits label may use holographic foil for security and gold for shelf presence. A pharmaceutical box may use small metallic marks for anti-counterfeit features. Consumer electronics packaging often uses silver foil on dark board for a premium tech look. Daily chemical tubes, bottle caps, and appliance panels rely on the same process for fine graphics and borders, where the foil has to survive handling and abrasion rather than shelf light alone. Hot stamping can struggle on rough, porous, or heavily recycled stocks. It can add cost on short runs because of tooling and setup. Metallized layers can complicate some recycling streams, so brands ask about substrate and foil compatibility. Clean spacing and strong contrast usually age better than a busy layout with tiny reversed type.
Most stamping problems look like a foil problem first and turn out to be a system problem. Replacing the foil rarely settles the issue on its own, because the cause usually sits in the layers underneath the foil, in the printed surface, or in the press setup. Several causes can stack on top of each other. Check the whole process for obvious faults first, then change one controlled variable at a time and record the result.
Common defects tend to cluster:
Poor release, often pointing to temperature, dwell, or a release coat mismatch.
Ragged edges, which can come from low pressure, worn dies, or substrate compressibility.
Spotty transfer, which may involve surface contamination, static, or uneven board.
Poor rub resistance, which can trace to adhesive choice, overlamination, or handling too soon.
A disciplined converter checks substrate surface energy, die face temperature, dwell, pressure, and post-press stress before blaming the foil. That order saves time and material.
For demanding packaging work, the foil is only one part of the system. A supplier that understands coating chemistry, release behavior, and substrate interaction can shorten the trial loop. GL Foils supplies HP1 conventional and HP2 holographic hot-stamping foils for paper and paperboard, including grades for fine lines, larger areas, overprinting and special optical effects. Plastic substrates require a separately matched foil grade rather than a paper-foil specification. Manufacturing capacity and supply chain discipline help keep demanding projects moving, and technical support reaches clients worldwide. For packaging teams dealing with tricky boards, low-energy films, or tight release windows, that kind of depth can matter as much as the foil shade on the swatch.

2026/10/28
Gold foil can be stamped on selected UV-varnished cartons, but the surface and foil must match. Learn what to check before approving a finished box.

2026/10/26
Gold foil can look perfect on a flat carton and crack after folding. See what to check in the artwork, board, crease and finished sample.

2026/10/26
Holographic foil and hologram technology add layered authentication to packaging, supporting brand protection with verifiable optical security.

2026/10/23
Holographic foil and hot stamping elevate packaging perceived value with consistent optical effects for premium cartons.

2026/10/22
Holographic paper for cosmetic cartons adds light-shifting effects, foil stamping performance, and premium shelf appeal for beauty packaging.

